 French
 English
 Dutch

The Scalable Agitated Baffle Reactor (SABRe) combines the flexibility of batch processing with the performance characteristics of flow chemistry. The system exists as a multipurpose, scalable reactor that retains the engineering advantages of batch reactors while providing heat and mass transfer performance that is comparable to tubular and chip reactors.
By combining these approaches, SABRe supports higher product quality, faster process development, and increased throughput.
Designed for rapid scale-up
SABRe provides a straightforward route from laboratory-scale experiments to pilot and production-scale manufacturing. The system is suitable for:
- Rapid process scale-up
- Accelerating complex and exothermic processes
- Process intensification with high throughput at low cost
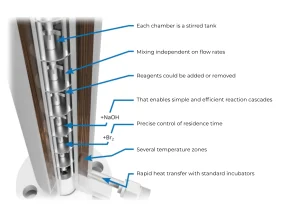
The reactor reimagines a series of continuous stirred-tank reactors (CSTRs) in a simple, modular, and scalable design.
Modular design for versatile applications
SABRe is designed as a drop-in replacement for jacketed batch reactors, making it compatible with major laboratory pumps, heaters, chillers, and overhead stirrers. This allows users to investigate continuous manufacturing without investing in an entirely new equipment platform.
A single pressure vessel can be configured with different options, including:
- Multiple reactor volumes
- Different impeller designs
- Various inlet and outlet positions
- Different numbers of reaction chambers
- Alternative baffle geometries
The use of a removable insert enables these configurations.
Precise reaction control from lab to production
 SABRe maintains consistent reaction control, including at long residence times and larger production scales. Because mixing is independent of pumping rates, the reactor provides consistent, controllable, and predictable mass transfer performance.
Several jacket options are available to achieve high heat transfer rates, making the system suitable for hazardous and exothermic reactions.
The SABRe platform is available in three standard sizes for laboratory, pilot, and production-scale applications, providing a clear scale-up pathway while maintaining yield, product purity, and energy efficiency.
Proven performance
SABRe has been evaluated in liquid-liquid enzymatic esterification processes, where its performance has been compared with batch reactors, chip reactors, and other agitated continuous reactor systems.
Technical features
| Primary wetted material | • 316 Stainless Steel • C276 Hastelloy • Glass or quartz |
|---|---|
| Secondary wetted material | PTFE / FFKM |
| Reactor volume | Lab: 30–120 mL Pilot: 1.0–10 L Production: 10–100 L |
